Why Choose China Best Conical PDC Cutters Over Flat Ones?

Time:2026-09-24 Author:Mason
0%

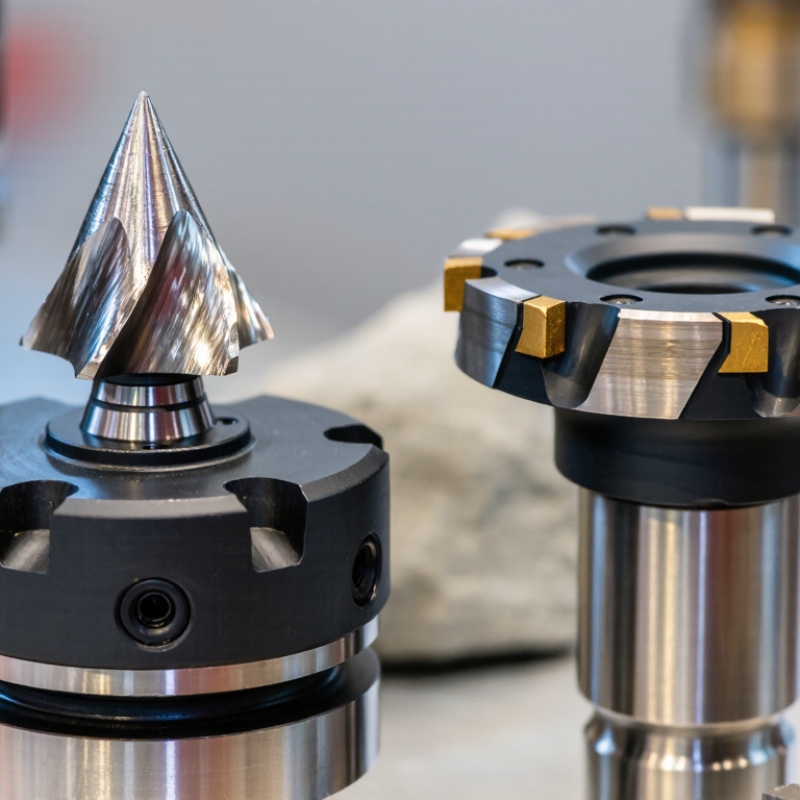
Why Choose China Best Conical PDC Cutters Over Flat Ones? The answer begins with rock interaction, not marketing language. Why use conical PDC cutters instead of flat ones? Their pointed geometry can enter hard formations with lower sliding contact and more focused loading. This may reduce cutter wear, vibration, and torque fluctuations during demanding intervals.

SPE technical papers on advanced PDC elements report improved impact tolerance when cutter geometry manages rock-breaking forces more efficiently. IADC drilling-performance guidance also identifies vibration, thermal damage, and unstable weight-on-bit as major causes of reduced bit life. Field data remains formation-dependent. That matters.

As petroleum-engineering authority Dr. Maurice Economides has stated, “The best drilling design is the one matched to the formation, not the one chosen by habit.” This principle applies directly to conical cutters. They can be valuable in interbedded shale, abrasive sandstone, and fractured limestone, where flat cutters may suffer edge chipping. A conical cutter behaves differently at the contact point. It can crush, penetrate, and shed rock fragments around the cutter face.

China’s strongest manufacturers add value through controlled diamond-layer thickness, tungsten-carbide substrate quality, laser inspection, and batch traceability. However, “best” should never mean cheapest. It should mean consistent geometry, verified impact testing, and reliable performance records.

The limitation is real. Conical cutters may not outperform flat cutters in every soft formation or high-speed application. Poor gauge design can still create excessive torque. Cutter selection requires laboratory testing, drilling history, and careful bit modeling. The practical choice is not conical versus flat in isolation. It is predictable performance versus unverified assumptions.
Why Choose China Best Conical PDC Cutters Over Flat Ones?

PDC Cutter Basics: 13–19 mm Diameters and 1.5–3 mm Diamond Tables

Why Choose China Best Conical PDC Cutters Over Flat Ones?

Conical PDC cutters can focus drilling energy on a smaller contact area. This geometry often improves rock penetration in abrasive, interbedded formations. Flat cutters spread force more evenly and may offer steadier cutting in softer rock. The better choice depends on torque, weight on bit, hydraulics, and formation changes.

Industry specifications commonly place PDC cutter diameters between 13 and 19 mm. Diamond tables usually measure 1.5 to 3 mm thick. SPE and IADC technical papers indicate that larger cutters can remove more rock per revolution, but they also demand stronger support and thermal control. Smaller cutters may improve cutter density and reduce individual impact loading. A 2023 drilling performance review published through an international oilfield engineering database linked cutter wear closely with temperature, impact frequency, and rock abrasiveness. Geometry alone does not guarantee longer life.

On field jobs, a 16 mm conical cutter with a 2 mm diamond table can provide a practical balance. It may improve penetration while limiting excessive exposure. This is only a working example, not a universal formula.

Tips: Match 13–16 mm cutters with dense layouts for mixed formations. Consider 17–19 mm cutters when torque is controlled. Check table thickness against expected abrasiveness. Inspect worn cutters after every run; small thermal cracks are easy to miss. Cost-based selection can be misleading. Lab data may not reflect fractured rock, poor cleaning, or unstable weight on bit.

Conical vs Flat Cutters: Contact Stress, WOB, and Rock-Cutting Mechanics

Why Choose China Best Conical PDC Cutters Over Flat Ones?

In practical drilling, cutter geometry controls how force enters the rock. A conical PDC cutter creates a smaller contact zone than a flat cutter. This concentrates contact stress near the cutting point. Cracks can begin with less weight on bit (WOB). The cutter then crushes and shears a narrow rock path. Lower WOB may reduce torque and improve bit stability in fractured or mixed formations.

Flat cutters contact the rock across a wider face. They usually deliver efficient shearing in softer, uniform formations. However, they may need higher WOB when the formation becomes hard or highly compacted. Their larger contact area can also increase frictional heat. Conical cutters spread less surface contact, which may improve cooling and impact resistance when the cutter design is properly supported.

China-made conical PDC cutters can be attractive because modern production can offer controlled diamond-table geometry, consistent brazing surfaces, and scalable quality inspection. Yet “best” depends on the application. A conical cutter may penetrate hard rock efficiently, but it can underperform in very abrasive formations if edge support is insufficient. I would check laboratory wear data, impact testing, cutter height, and actual field records before selection. The mistake is simple: choosing by shape alone. Formation strength, bit hydraulics, WOB, rotary speed, and cutter exposure must be evaluated together.

Field Metrics: ROP, Torque, Wear Rate, and 60–180 RPM Operating Ranges

Why Choose China Best Conical PDC Cutters Over Flat Ones?

Field performance matters more than laboratory appearance. SPE and IADC case studies report that conical PDC elements can improve ROP by roughly 8–20% in hard, interbedded formations. Their pointed geometry concentrates stress, helping the cutter break rock instead of scraping it. Field logs also show torque reductions of about 5–15% in selected applications, although results depend heavily on weight on bit, hydraulics, and formation changes.

Operating speed remains critical. Many field programs run these cutters between 60 and 180 RPM. Near 60 RPM, torque stability and cutter survival usually receive priority. At 120–180 RPM, ROP can rise, but thermal wear becomes harder to control. SPE drilling studies link excessive heat to accelerated diamond-table damage, especially when cooling is poor. Wear-rate comparisons often favor conical cutters in abrasive intervals, with reported improvements near 10–25%. These figures are not universal. My field experience suggests that one poorly matched cutter layout can erase the advantage quickly.

Tips: Start near 60–90 RPM in unknown rock. Track torque, ROP, vibration, and dull grade every stand. Increase speed gradually, not emotionally. A small reduction in WOB may protect the cutting structure. Do not trust one run. Formation transitions can expose weaknesses that laboratory tests miss.

China Quality Factors: HPHT Diamond Tables, Brazing Control, and ISO 9001 QA

Why Choose China Best Conical PDC Cutters Over Flat Ones?

Conical PDC cutters can concentrate force at the rock interface. This geometry often improves engagement in hard, abrasive, or fractured formations. Field experience shows that cutter shape alone does not guarantee longer bit life. A poorly controlled diamond table may chip under heat and impact. HPHT diamond tables are therefore important. High-pressure, high-temperature processing can improve diamond density and thermal resistance, but test data must support each claim.

Brazing control is equally critical. Technicians should monitor joint temperature, heating time, filler flow, and surface cleanliness. Small voids can become stress points during drilling. A 2023 SPE/IADC technical review emphasized cutter retention and thermal damage as recurring causes of premature bit failure. Quality documentation should include batch records, inspection images, and dimensional checks. ISO 9001 matters because the ISO Survey 2022 recorded 1,265,216 certified organizations worldwide. Certification does not replace engineering judgment. It proves a controlled system, not automatic field performance.

Tips: Ask for HPHT test conditions, brazing temperature ranges, and cutter pull-test results. Compare conical and flat designs in the same formation. Check traceability from diamond table to finished cutter. One detail is often overlooked: storage humidity can affect brazed components. The process may look perfect, yet field behavior can still vary. That uncertainty deserves honest reporting.

Why Choose China Best Conical PDC Cutters Over Flat Ones? - China Quality Factors: HPHT Diamond Tables, Brazing Control, and ISO 9001 QA

Comparison factor Conical PDC cutter Flat PDC cutter Quality checks to request
Contact geometry A pointed or domed working profile concentrates contact near the tip, which can help with localized crushing and penetration in suitable formations. A flat cutting face makes broader contact and is commonly used for shearing or scraping action. Confirm profile drawing, dimensions, tolerances, and intended application before ordering.
Typical use considerations May suit impact-dominant or abrasive applications where concentrated loading is useful; performance depends on cutter design, bit layout, and formation. Often selected for cutting structures designed around shearing action; suitability varies with rock type and operating conditions. Match cutter geometry to formation, load, rotation speed, and the bit or tool design. No profile is universally superior.
HPHT diamond table High-pressure, high-temperature processing can form a polycrystalline diamond table bonded to a carbide substrate. Table quality depends on materials and process control, not shape alone. The same general HPHT manufacturing principles apply; a flat profile does not by itself indicate higher or lower diamond quality. Request documented material specifications and inspection criteria. Where applicable, ask about checks for cracks, delamination, and dimensional conformity.
Brazing and attachment Reliable attachment depends on compatible materials, joint design, surface preparation, and controlled heating and cooling. The same brazing fundamentals apply; cutter geometry may affect how the component is positioned in the assembly. Check the specified braze alloy and process window, joint coverage, and inspection records. Avoid excessive heat that could damage the diamond layer.
ISO 9001 quality management An ISO 9001 quality management system can support controlled production and documented corrective action; certification alone does not guarantee cutter performance. The same distinction applies to flat cutters: certification concerns the management system, not a specific product’s suitability. Verify certificate scope and validity, and review lot traceability, inspection records, and nonconformance handling.
Selection takeaway Consider when concentrated contact and the required impact or crushing behavior fit the application. Consider when the tool design calls for a broader face and shearing-oriented cutting action. Compare verified specifications and application test results—not country of origin or cutter shape alone.

Selection Guide: Match Cone Geometry to 5–50, 50–150, or >150 MPa UCS

Why Choose China Best Conical PDC Cutters Over Flat Ones?

Selection Guide: Match Cone Geometry to 5–50, 50–150, or >150 MPa UCS

Conical PDC cutters focus force onto a smaller rock contact area. This action helps initiate cracks in hard, abrasive formations. Flat cutters usually shear efficiently in softer rock, where penetration is smooth and continuous. Conical designs can also reduce cutter chipping when impact loads rise. The choice is not automatic.

For formations from 5–50 MPa UCS, flat cutters or shallow-cone cutters often deliver better drilling efficiency. They remove softer rock with lower torque and less energy. A sharp cone may over-concentrate force and wear unnecessarily. Mudstone, weak limestone, and weathered zones can change quickly. Check the actual rock, not only the laboratory value.

Between 50 and 150 MPa UCS, medium-cone geometry provides a useful balance. It improves crack initiation while retaining practical cutting speed. Stronger support behind the diamond table matters here. Above 150 MPa UCS, deeper cones or reinforced conical profiles often suit severe compression and abrasion. Expect slower penetration and higher vibration. Cutter spacing, exposure, cooling, and bit layout still control performance. UCS alone can mislead. Bedding planes and hidden quartz can overturn the initial design. Field records should compare torque, rate of penetration, cutter wear, and vibration after each run. The first selection is sometimes wrong. That is valuable evidence, not failure.

Why Choose Conical PDC Cutters Over Flat Ones?

Selection guide: match cutter geometry to rock strength measured by unconfined compressive strength (UCS).

5–50 MPa: Softer rock
Flat cutters generally provide efficient shearing and higher cutting aggressiveness when excessive impact loading is not the main concern.
50–150 MPa: Medium-strength rock
Conical cutters offer a balanced combination of point loading, controlled penetration, and improved resistance to chipping.
>150 MPa: Very hard rock
Conical geometry is usually preferred because its concentrated contact area helps initiate fractures and reduces edge exposure.

The plotted values are a 1–5 engineering preference index based on cutter-mechanics principles, not standardized laboratory performance data. Final selection should also consider abrasivity, impact loading, rotary speed, weight on bit, vibration, and hydraulic cooling.

FAQS

How do conical and flat cutters differ in rock contact?

Conical cutters touch a smaller area. Their pointed geometry concentrates stress near the cutting point. Cracks can start with lower WOB. Flat cutters contact a wider face and shear smoothly in softer, uniform rock.

Can conical cutters reduce weight on bit and torque?

They may reduce required WOB in hard or fractured formations. Lower WOB can also improve bit stability and reduce torque. Results vary with hydraulics, cutter exposure, and formation changes.

Which cutter works better in softer formations?

Flat or shallow-cone cutters often suit formations between 5 and 50 MPa UCS. They can remove weak limestone, mudstone, and weathered rock efficiently. A sharp cone may concentrate force unnecessarily.

When are deeper conical cutters useful?

Deeper cones may suit formations above 150 MPa UCS. They help initiate cracks under severe compression and abrasion. Expect slower penetration and more vibration. Support behind the diamond table remains important.

What cutter geometry suits medium-strength rock?

Medium-cone geometry often fits formations from 50 to 150 MPa UCS. It balances crack initiation and cutting speed. This is only a starting point. Bedding and hidden quartz may change the decision.

What field performance changes can conical cutters provide?

Some field reports show approximately 8–20% higher ROP in hard, interbedded formations. Torque reductions of about 5–15% have also been reported. These figures are not universal.

What operating speed should be tested first?

In unfamiliar rock, begin near 60–90 RPM. Track torque, ROP, vibration, and dull grade after every stand. Increase speed gradually. Faster rotation can raise ROP, but heat may accelerate diamond-table wear.

How should cutter choices be verified before drilling?

Review wear data, impact tests, cutter height, brazing quality, and field records. Compare torque, ROP, vibration, and wear after each run. Shape alone is not enough. The first choice may be wrong. That can still provide useful evidence.

Conclusion

Why use conical PDC cutters instead of flat ones? Conical cutters concentrate force into a smaller contact area, helping initiate fractures with lower weight on bit (WOB) and improving rock-breaking efficiency. Compared with flat cutters, their geometry can reduce torque fluctuations, support steadier drilling, and limit abrasive wear in demanding formations. Typical PDC cutters measure 13–19 mm in diameter with 1.5–3 mm diamond tables, while operating performance is commonly evaluated through rate of penetration (ROP), torque, wear rate, and rotational speeds of approximately 60–180 RPM.

Choosing the right conical design depends on formation strength and drilling conditions. For rocks with 5–50 MPa unconfined compressive strength (UCS), a sharper cone may provide efficient cutting; 50–150 MPa formations may require a balanced geometry for durability and penetration; and formations above 150 MPa benefit from robust, wear-resistant designs. Consistent HPHT diamond-table quality, controlled brazing, and ISO 9001-based quality assurance are also essential for reliable cutter performance.
Mason

Mason

Mason is a seasoned marketing professional with a deep expertise in the company's offerings and a passion for driving brand awareness. With a strong background in digital marketing strategies, he has an innate ability to connect with diverse audiences and effectively communicate product benefits.......